Pressure Safety Valve: Selection and Applications
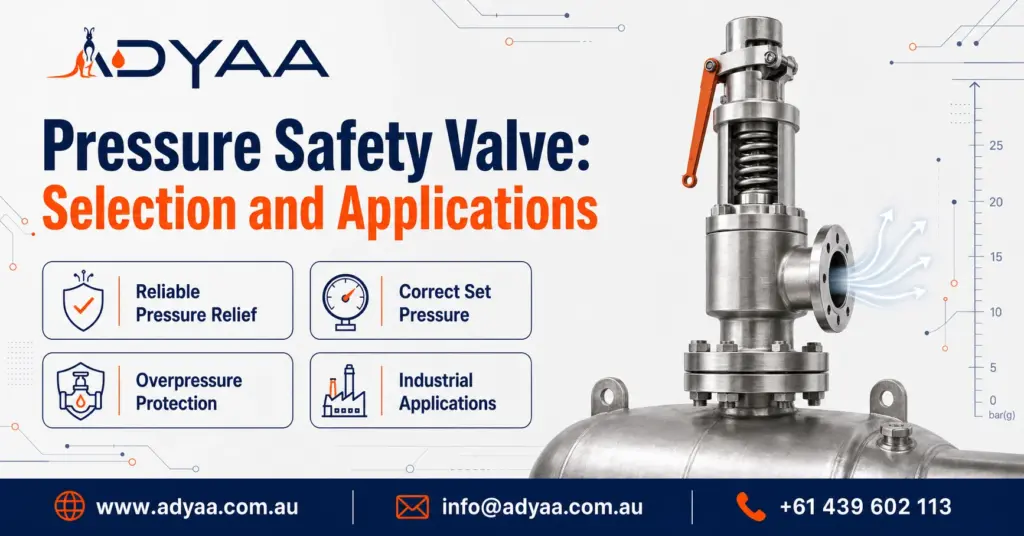
Pressure Safety Valve: Selection and Applications Industrial systems often operate under high pressure, making reliable pressure protection essential. A Pressure Safety Valve automatically releases excess pressure before it reaches unsafe levels, helping protect equipment, personnel and production processes. From pressure vessels and boilers to pipelines and storage systems, these valves play a critical role in maintaining safe and efficient industrial operations. What Is a Pressure Safety Valve? A Pressure Safety Valve is a mechanical safety device designed to automatically open when system pressure exceeds a predetermined set point. Once the pressure returns to a safe operating range, the valve closes automatically, allowing the system to continue operating normally. Pressure safety valves are commonly installed on pressure vessels, boilers, compressors, pipelines and process equipment where overpressure could damage assets or interrupt production. Why Pressure Safety Valves Matter Pressure safety valves are a key component of industrial pressure protection systems. Protect Equipment Prevent excessive pressure from damaging valuable industrial assets. Improve Plant Safety Help reduce the risks associated with overpressure conditions. Reduce Downtime Minimise equipment failures and unexpected production interruptions. Support Regulatory Compliance Assist industries in meeting recognised pressure protection practices. Maintain Process Stability Keep pressure within safe operating limits during process fluctuations. Extend Equipment Life Reduce stress on equipment and improve long-term reliability. How a Pressure Safety Valve Works Although designs vary, most pressure safety valves follow the same operating principle. The valve remains closed during normal operating conditions. System pressure gradually increases. When the preset pressure is reached, the valve automatically opens. Excess pressure is safely discharged. Once pressure returns to an acceptable level, the valve reseats and closes. This automatic operation helps protect both equipment and personnel without requiring manual intervention. Types of Pressure Safety Valves Different industrial applications require different valve designs. Spring Loaded Safety Valves The most common design, using a calibrated spring to control the opening pressure. Pilot Operated Safety Valves Designed for high-pressure applications requiring accurate pressure control and reduced leakage. Threaded Safety Valves Suitable for compact process systems and smaller pipe sizes. Flanged Safety Valves Used in larger industrial installations where higher flow capacity is required. Hygienic Safety Valves Designed for food, beverage and pharmaceutical applications requiring sanitary construction. Cryogenic Safety Valves Used in low-temperature applications involving liquefied gases and cryogenic systems. Pressure Safety Valve vs Pressure Relief Valve Although the terms are often used interchangeably, there are operational differences. Feature Pressure Safety Valve Pressure Relief Valve Primary Purpose Protect against overpressure Control excess system pressure Opening Action Opens rapidly at set pressure Opens gradually as pressure increases Typical Applications Steam, gas and compressed air Liquid systems Closing Action Automatically reseats Gradually closes as pressure decreases Selecting the correct valve depends on the process media, operating conditions and application requirements. Where Pressure Safety Valves Are Used Pressure safety valves protect a wide range of industrial processes. Oil & Gas Protect pipelines, separators and pressure vessels operating under high pressure. Chemical Processing Prevent excessive pressure in reactors, tanks and processing equipment. Manufacturing Protect compressed air systems, hydraulic equipment and industrial machinery. Food & Beverage Maintain pressure protection in hygienic processing systems. Pharmaceutical Support controlled pressure conditions during production processes. Power Generation Protect boilers, steam systems and pressure vessels. Water & Wastewater Safeguard pumps, pipelines and pressure systems. Mining Protect high-pressure process equipment operating in demanding environments. Pressure Safety Valve Selection Checklist Before selecting a pressure safety valve, consider the following: ✔ Operating pressure ✔ Set pressure ✔ Process media ✔ Flow capacity ✔ Operating temperature ✔ Valve connection type ✔ Material compatibility ✔ Installation orientation ✔ Industry standards ✔ Maintenance requirements Selecting the correct valve improves both operational reliability and long-term equipment protection. Common Mistakes When Selecting Pressure Safety Valves Improper valve selection can affect both safety and performance. Common mistakes include: Selecting an incorrect pressure setting Choosing the wrong valve size Ignoring process media compatibility Using unsuitable materials Incorrect installation Delaying inspection and maintenance Overlooking discharge capacity requirements Working with experienced pressure protection specialists helps minimise these risks. Why Pressure Safety Valves Are Important Overpressure events can occur unexpectedly due to equipment failures, thermal expansion, blocked outlets or control system malfunctions. A properly selected Pressure Safety Valve provides automatic protection, helping reduce equipment damage, production losses and maintenance costs while supporting safer plant operations. Why Choose ADYAA? ADYAA supplies pressure protection solutions for industrial applications across Australia. Comprehensive Pressure Protection Solutions Safety Valves, Rupture Discs, Tank Protection Systems and related accessories. Technical Product Selection Support in selecting valves based on process conditions and industry requirements. Quality Industrial Products Solutions designed for reliable performance in demanding environments. Industry Experience Supporting a wide range of industrial process applications. Australia-wide Support Reliable assistance for industries across Australia. Long-Term Performance Helping improve operational safety, equipment protection and process reliability. Frequently Asked Questions What is a Pressure Safety Valve? A Pressure Safety Valve automatically releases excess pressure to protect industrial equipment from overpressure conditions. Where are Pressure Safety Valves used? They are commonly used in boilers, pressure vessels, pipelines, compressors and industrial process equipment. What causes a Pressure Safety Valve to open? The valve opens automatically when system pressure exceeds its preset operating pressure. What is the difference between a Pressure Safety Valve and a Relief Valve? Safety valves generally open rapidly for gas or steam applications, while relief valves usually open progressively for liquid systems. How often should Pressure Safety Valves be inspected? Inspection intervals depend on operating conditions, industry standards and maintenance programs. How do I choose the right Pressure Safety Valve? Selection depends on operating pressure, process media, temperature, flow capacity, material compatibility and applicable industry standards. A Pressure Safety Valve is one of the most important components of any industrial pressure protection system. Choosing the right valve helps improve process safety, protect valuable equipment and maintain reliable plant operations. ADYAA supplies industrial pressure safety solutions designed to support a wide range of process applications across Australia. Need help selecting the right Pressure Safety Valve? Our team can help you choose the right pressure protection
Burst Disk Indicators: Improving Plant Safety
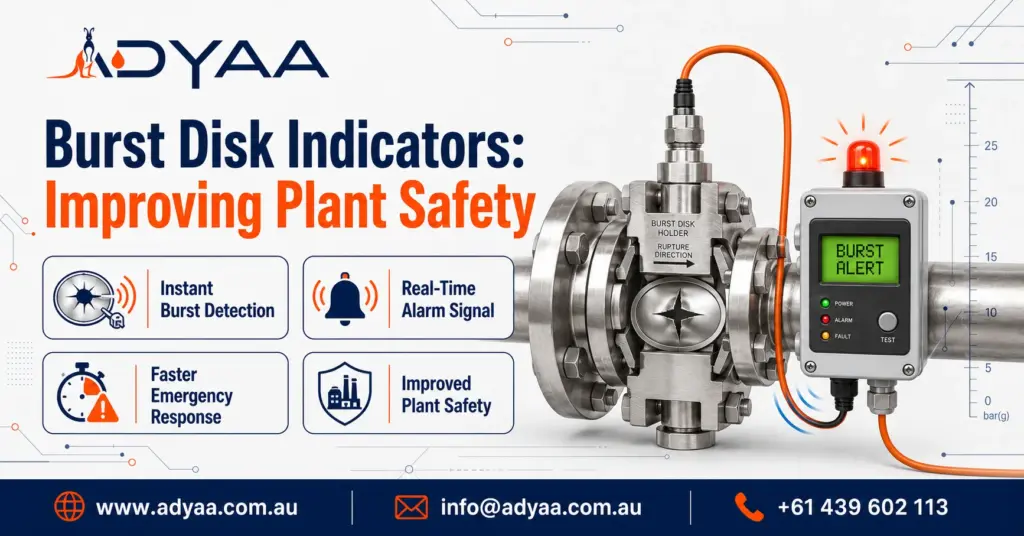
Burst Disk Indicators: Improving Plant Safety A rupture disc provides reliable protection against overpressure, but once it bursts, operators need to know immediately. A Burst Disk Indicator continuously monitors the condition of a rupture disc and instantly signals when the disc has activated. This allows maintenance teams to respond quickly, minimise downtime and restore normal operations as soon as possible. From chemical processing plants to power generation facilities, burst disk indicators improve process visibility while supporting safer and more efficient industrial operations. What Is a Burst Disk Indicator? A Burst Disk Indicator is an electronic monitoring device used with a rupture disc to detect when the disc has burst. During normal operation, the monitoring circuit remains intact. When the rupture disc activates because of an overpressure event, the electrical circuit changes state, sending an alarm or signal to the plant’s control system. This immediate notification helps operators identify pressure events without manually inspecting the rupture disc. Why Burst Disk Indicators Matter Adding a burst disk indicator improves both plant safety and operational efficiency. Immediate Burst Detection Receive instant notification when a rupture disc activates. Reduce Downtime Allow maintenance teams to respond quickly after a pressure event. Improve Plant Safety Reduce the time equipment operates after rupture disc activation. Support Remote Monitoring Transmit alarm signals directly to PLC and SCADA systems. Improve Maintenance Planning Identify activated rupture discs without manual inspections. Increase Operational Reliability Provide continuous monitoring of pressure protection devices. How a Burst Disk Indicator Works Burst disk indicators continuously monitor the rupture disc during operation. The rupture disc remains intact during normal operating conditions. The burst disk indicator monitors the electrical circuit. An overpressure event causes the rupture disc to burst. The monitoring circuit changes state. An alarm is sent to the control room, PLC or SCADA system. Maintenance personnel replace the rupture disc and restore the system. This simple monitoring method improves response times following overpressure events. Types of Burst Disk Indicators Different monitoring solutions are available depending on plant requirements. Electrical Burst Disk Indicators Monitor the rupture disc using electrical continuity. Intrinsically Safe Indicators Designed for hazardous area applications where explosion protection is required. PLC Integrated Indicators Provide direct communication with industrial automation systems. Remote Monitoring Indicators Allow operators to monitor rupture disc status from central control rooms. Visual Indicator Systems Provide local visual confirmation after rupture disc activation. Smart Monitoring Systems Support advanced diagnostics and integration with modern industrial networks. Burst Disk Indicator Comparison Type Best For Typical Application Electrical General Industry Manufacturing Intrinsically Safe Hazardous Areas Oil & Gas PLC Integrated Automation Process Plants Remote Monitoring Central Control Large Facilities Visual Indicator Local Monitoring Storage Tanks Smart System Industry 4.0 Advanced Manufacturing Where Burst Disk Indicators Are Used Burst disk indicators are widely used wherever rupture discs protect critical equipment. Oil & Gas Monitor rupture discs installed on pressure vessels and process equipment. Chemical Processing Provide immediate notification following pressure relief events. Petrochemical Support continuous monitoring of pressure protection systems. Pharmaceutical Monitor sterile process equipment while maintaining system integrity. Food & Beverage Support pressure protection in hygienic production systems. Power Generation Monitor boilers, steam systems and pressure vessels. Water & Wastewater Protect chemical dosing and pressurised treatment systems. Manufacturing Improve equipment monitoring and maintenance response times. Burst Disk Indicator Selection Checklist Before selecting a burst disk indicator, consider: ✔ Rupture disc type ✔ Electrical compatibility ✔ Control system integration ✔ Hazardous area requirements ✔ Operating temperature ✔ Environmental conditions ✔ Alarm requirements ✔ Cable routing ✔ Maintenance accessibility ✔ Industry standards Choosing the correct monitoring system improves safety and operational reliability. Common Mistakes When Selecting Burst Disk Indicators Common issues include: Selecting an incompatible indicator Ignoring hazardous area approvals Incorrect wiring Poor installation practices Failing to test alarm systems Delaying replacement after activation Not integrating with plant monitoring systems A properly designed monitoring system helps avoid these problems. Why Burst Detection Matters A rupture disc performs its job only once before it must be replaced. Without a burst disk indicator, operators may not immediately know that the disc has activated. Continuous monitoring helps reduce production delays, improve maintenance response times and ensure pressure protection systems are restored as quickly as possible. Why Choose ADYAA? ADYAA supplies pressure protection and monitoring solutions for industries across Australia. Complete Pressure Protection Portfolio Rupture Discs, Safety Valves, Tank Protection Systems and monitoring accessories. Technical Expertise Support in selecting compatible rupture disc monitoring solutions. Reliable Industrial Products Designed for demanding industrial operating environments. Automation Ready Compatible with PLC, SCADA and industrial control systems. Australia-wide Support Reliable technical assistance across Australia. Long-Term Reliability Helping industries improve pressure protection, monitoring and operational safety. Frequently Asked Questions What is a Burst Disk Indicator? A Burst Disk Indicator monitors a rupture disc and sends an alarm when the disc bursts during an overpressure event. Does a Burst Disk Indicator prevent overpressure? No. The rupture disc provides pressure protection, while the burst disk indicator detects when the rupture disc has activated. Can Burst Disk Indicators connect to PLC systems? Yes. Many models integrate directly with PLC, SCADA and other industrial automation systems. Where are Burst Disk Indicators commonly used? Oil & Gas, Chemical Processing, Pharmaceutical, Food & Beverage, Manufacturing, Power Generation and Water Treatment industries. Do Burst Disk Indicators require maintenance? Routine inspection and functional testing help ensure reliable operation. How do I choose the right Burst Disk Indicator? Selection depends on the rupture disc type, control system, operating environment, hazardous area requirements and monitoring needs. A Burst Disk Indicator improves the effectiveness of rupture disc systems by providing immediate notification when pressure relief occurs. Fast detection allows maintenance teams to restore equipment quickly, helping minimise downtime and maintain safe industrial operations. ADYAA supplies burst disk indicators, rupture discs and complete pressure protection solutions for industries across Australia, helping businesses improve safety, monitoring and operational reliability. Need help selecting the right Burst Disk Indicator? Our specialists can help you choose a compatible monitoring solution for your rupture disc and pressure protection system. Burst Disk
How to Choose the Right Pressure Transmitter for Industrial Applications
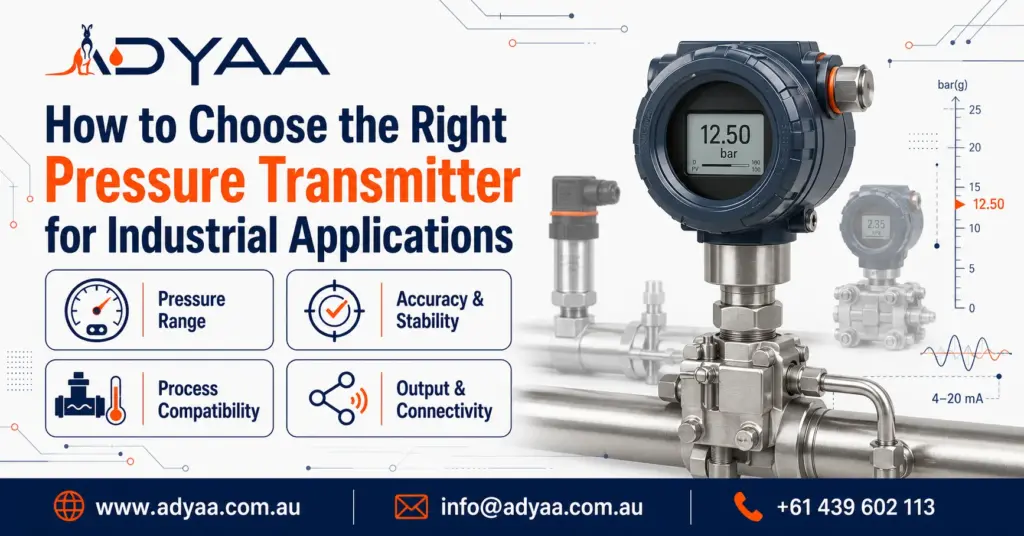
How to Choose the Right Pressure Transmitter for Industrial Applications Pressure transmitters are used across industries to monitor and control the pressure of liquids, gases and steam. However, selecting the right transmitter involves more than choosing a pressure range. Factors such as process media, operating conditions, accuracy requirements and communication protocols all influence performance. Choosing the right Pressure Transmitter helps improve process reliability, reduce maintenance requirements and support long-term operational efficiency. What Is a Pressure Transmitter? A pressure transmitter is an industrial instrument that measures process pressure and converts it into a standard electrical output for monitoring and control systems. Modern pressure transmitters provide continuous pressure measurements and integrate with PLC, SCADA and Distributed Control Systems (DCS), allowing operators to monitor critical processes in real time. They are commonly used in manufacturing, oil & gas, water treatment, chemical processing, mining, food & beverage and pharmaceutical industries. Why Choosing the Right Pressure Transmitter Matters Selecting the correct pressure transmitter helps improve overall plant performance. Improve Measurement Accuracy Accurate pressure readings support better process control and decision-making. Increase Equipment Reliability Using the right transmitter reduces unnecessary wear on equipment. Reduce Downtime Reliable pressure monitoring helps identify issues before they affect production. Improve Process Efficiency Consistent pressure measurements help optimise industrial operations. Support Automation Pressure transmitters provide reliable data for automated control systems. Lower Maintenance Costs Choosing the right instrument reduces unexpected failures and maintenance requirements. Factors to Consider When Choosing a Pressure Transmitter Selecting the right pressure transmitter requires evaluating several process conditions. Pressure Range Choose a transmitter with a pressure range that comfortably covers normal operating conditions without exceeding its limits. Process Media Consider whether the transmitter will measure water, chemicals, steam, gases, oils or corrosive fluids. The wetted materials must be compatible with the process media to ensure long-term reliability. Measurement Accuracy Applications such as pharmaceutical manufacturing and custody transfer often require higher accuracy than general industrial processes. Select a transmitter that matches the required level of measurement precision. Operating Temperature High or low process temperatures can affect transmitter performance. Verify that both the process temperature and ambient temperature fall within the instrument’s operating limits. Pressure Connection Ensure the pressure connection matches your piping or equipment. Common process connections include: BSP NPT Flanged Connections Hygienic Connections Output Signal Most industrial pressure transmitters support one or more communication methods. Common outputs include: 4–20 mA HART Modbus IO-Link PROFIBUS FOUNDATION Fieldbus Choose the communication protocol that integrates with your automation system. Environmental Conditions Consider installation conditions such as: Dust Moisture Vibration Hazardous Areas Outdoor Exposure The enclosure rating should suit the operating environment. Certification Requirements Certain industries require transmitters that comply with recognised standards or hazardous-area approvals. Confirm that the selected transmitter meets the applicable project or industry requirements. Pressure Transmitter Selection Checklist Selection Factor Why It Matters Pressure Range Prevents overloading and improves measurement accuracy Process Media Ensures material compatibility Accuracy Supports reliable process control Temperature Maintains stable performance Output Signal Enables seamless automation integration Process Connection Simplifies installation Environmental Rating Protects against harsh conditions Certifications Supports project compliance Industrial Applications Pressure transmitters are used in a wide variety of industries. Oil & Gas Monitor pipelines, separators, storage tanks and compressors. Chemical Processing Measure reactor, vessel and pipeline pressures. Water & Wastewater Monitor pumps, filters and distribution systems. Food & Beverage Control process pressure during production and cleaning operations. Pharmaceutical Maintain consistent process conditions during manufacturing. Mining Measure slurry transport, hydraulic systems and process equipment. Power Generation Monitor boilers, turbines and cooling systems. Manufacturing Support automation across production lines and industrial machinery. Common Mistakes When Selecting a Pressure Transmitter Many pressure measurement issues result from incorrect selection. Common mistakes include: Selecting an incorrect pressure range Ignoring media compatibility Choosing unsuitable wetted materials Overlooking temperature limitations Selecting the wrong communication protocol Incorrect installation location Skipping routine calibration Proper planning helps improve measurement reliability and extend equipment life. Why Professional Selection Matters Pressure transmitters are often installed in critical process applications where measurement accuracy directly affects safety, efficiency and product quality. Working with experienced instrumentation specialists helps ensure the transmitter matches the operating conditions, process requirements and automation system. The right selection reduces maintenance costs while improving long-term operational performance. Why Choose ADYAA? ADYAA supplies industrial pressure measurement solutions for customers across Australia. Extensive Pressure Instrumentation Range Pressure Transmitters, Pressure Gauges, Pressure Switches and Pressure Accessories. Technical Product Expertise Support in selecting the right pressure measurement solution for your application. Reliable Industrial Products Solutions designed for demanding industrial environments. Automation Ready Compatible with PLC, SCADA and DCS platforms. Australia-wide Support Reliable technical assistance across Australia. Long-Term Process Reliability Helping industries improve measurement accuracy and operational efficiency. Frequently Asked Questions What pressure range should I choose? The transmitter should cover your normal operating pressure while allowing sufficient margin for temporary pressure fluctuations. Which output signal is most commonly used? The 4–20 mA output remains one of the most widely used standards in industrial automation, while HART, Modbus and IO-Link are also common. Can one pressure transmitter measure all process fluids? No. Material compatibility must be evaluated based on the process media and operating conditions. How accurate should a pressure transmitter be? The required accuracy depends on the application. General industrial processes and precision manufacturing may have different accuracy requirements. How often should pressure transmitters be calibrated? Calibration intervals depend on the application, operating conditions and maintenance programme. Can pressure transmitters be installed outdoors? Yes. Many industrial models are designed for outdoor use when installed with the appropriate environmental protection. Selecting the right Pressure Transmitter is essential for achieving accurate pressure measurement, reliable process control and efficient industrial operations. By considering pressure range, media compatibility, environmental conditions and communication requirements, businesses can improve equipment performance while reducing maintenance and downtime. ADYAA provides industrial pressure transmitters and instrumentation solutions across Australia, helping businesses select reliable products for a wide range of industrial applications. Need help choosing the right Pressure Transmitter? Our instrumentation specialists can help you select a pressure transmitter that matches your process conditions,
Tank Safety Systems: Protecting Industrial Storage Tanks
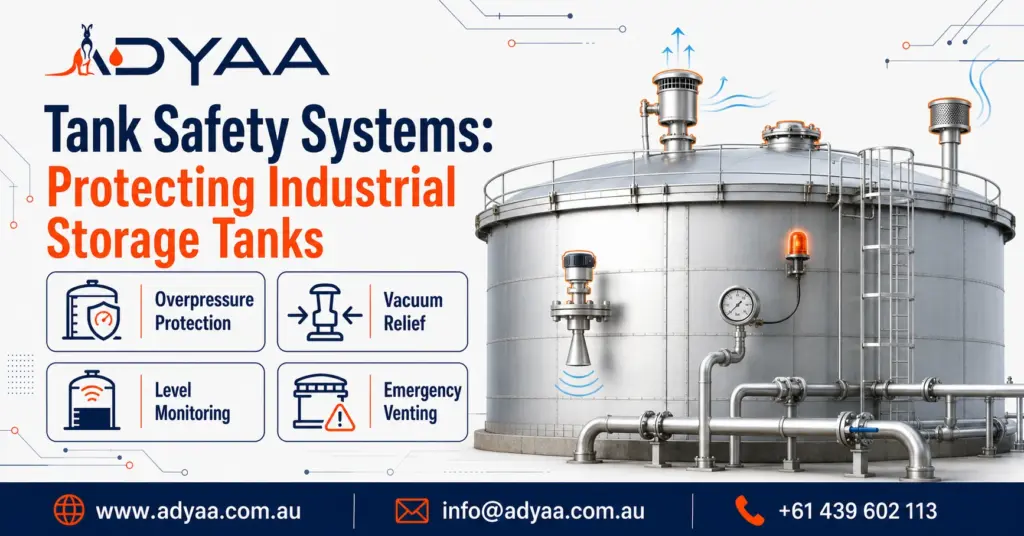
Tank Safety Systems: Protecting Industrial Storage Tanks Industrial storage tanks are designed to safely contain liquids, chemicals and gases under varying operating conditions. However, changes in pressure, vacuum or ignition sources can threaten both equipment and personnel. A Tank Safety System combines multiple protection devices to safeguard storage tanks, maintain process integrity and support safe plant operations. From fuel terminals and chemical plants to food processing facilities, effective tank safety systems play an important role in preventing equipment damage, reducing operational risks and improving long-term reliability. What Is a Tank Safety System? A Tank Safety System is a combination of pressure protection devices that help maintain safe operating conditions inside storage tanks. These systems are designed to control pressure changes caused by filling, emptying, temperature fluctuations or process operations while also reducing the risk of fire and equipment damage. A typical tank safety system may include: Pressure Vacuum Vents Emergency Relief Valves Flame Arrestors Blanket Gas Regulators Level Instrumentation Pressure Monitoring Devices Together, these components help protect both the storage tank and the surrounding facility. Why Tank Safety Systems Matter Proper tank protection improves both operational safety and equipment reliability. Protect Storage Tanks Prevent excessive pressure or vacuum from damaging tanks. Improve Plant Safety Reduce the risks associated with pressure build-up and ignition hazards. Minimise Product Loss Help reduce evaporation losses and product release. Support Reliable Operations Maintain stable operating conditions during filling and emptying. Extend Equipment Life Reduce mechanical stress on tanks and associated equipment. Improve Process Efficiency Support continuous and reliable plant operations. How a Tank Safety System Works Tank safety systems continuously respond to changing operating conditions. Product enters or leaves the storage tank. Internal pressure or vacuum changes. Protection devices monitor these changes. Pressure or vacuum is safely relieved when required. The tank returns to its normal operating condition. This automatic protection helps maintain safe operating conditions without interrupting production. Key Components of a Tank Safety System A complete tank safety solution typically includes several protection devices. Pressure Vacuum Vents Protect tanks against excessive internal pressure and vacuum during normal operation. Emergency Relief Valves Provide additional pressure relief during abnormal operating conditions such as fire exposure or rapid filling. Flame Arrestors Prevent flames from entering or travelling through tank vent systems. Blanket Gas Regulators Maintain protective inert gas pressure inside storage tanks. Pressure Monitoring Instruments Continuously monitor tank pressure and operating conditions. Level Measurement Instruments Measure tank levels to support safe storage operations and inventory management. Tank Safety System Components Comparison Component Primary Function Typical Application Pressure Vacuum Vent Pressure & Vacuum Protection Storage Tanks Emergency Relief Valve Emergency Pressure Relief Chemical Tanks Flame Arrestor Flame Protection Fuel Storage Blanket Gas Regulator Inert Gas Control Chemical Processing Pressure Instruments Pressure Monitoring Process Industries Level Transmitters Inventory Monitoring Tank Farms Where Tank Safety Systems Are Used Tank protection is essential across many industries. Oil & Gas Protect fuel storage tanks, terminals and processing facilities. Chemical Processing Safeguard chemical storage tanks against pressure changes. Petrochemical Support safe storage of volatile process media. Food & Beverage Protect storage vessels used for ingredients and finished products. Pharmaceutical Maintain controlled storage environments. Water & Wastewater Protect chemical dosing and storage tanks. Mining Monitor reagent storage tanks and processing facilities. Power Generation Protect fuel storage and process tanks. Tank Safety System Selection Checklist Before selecting a tank safety system, evaluate: ✔ Tank size ✔ Stored product ✔ Operating pressure ✔ Vacuum requirements ✔ Filling and emptying rates ✔ Venting capacity ✔ Hazard classification ✔ Environmental conditions ✔ Industry standards ✔ Maintenance accessibility Choosing the correct protection devices improves safety, equipment reliability and operational efficiency. Common Mistakes When Designing Tank Safety Systems Poor tank protection can increase operational risks. Common mistakes include: Undersized venting devices Ignoring vacuum protection Incorrect flame arrestor selection Poor equipment sizing Inadequate pressure monitoring Delayed maintenance Ignoring future process expansion A properly engineered system helps reduce these risks. Why Tank Protection Matters Storage tanks are continuously exposed to changing operating conditions. Even routine filling or temperature changes can create pressure or vacuum conditions capable of damaging equipment. A well-designed Tank Safety System helps maintain safe operating conditions, protects valuable assets and supports uninterrupted industrial operations. Why Choose ADYAA? ADYAA supplies complete tank protection solutions for industrial facilities across Australia. Comprehensive Tank Protection Solutions Pressure Vacuum Vents, Emergency Relief Valves, Flame Arrestors and related safety products. Technical Expertise Support in selecting the right protection solution for your storage application. Reliable Industrial Products Designed for demanding industrial operating environments. Integrated Safety Solutions Products compatible with modern process instrumentation and control systems. Australia-wide Support Reliable assistance for customers across Australia. Long-Term Equipment Protection Helping industries improve safety, reliability and operational performance. Frequently Asked Questions What is a Tank Safety System? A Tank Safety System protects storage tanks from excessive pressure, vacuum and fire-related hazards using specialised safety devices. What components are included in a Tank Safety System? Common components include Pressure Vacuum Vents, Emergency Relief Valves, Flame Arrestors, Blanket Gas Regulators and monitoring instruments. Why is vacuum protection important? Vacuum conditions can cause storage tanks to collapse if they are not properly protected. Where are Tank Safety Systems used? Oil & Gas, Chemical Processing, Petrochemical, Water Treatment, Food & Beverage, Mining and Pharmaceutical industries. How do I choose the right Tank Safety System? Selection depends on tank size, stored product, operating conditions, venting requirements and applicable engineering standards. Do Tank Safety Systems require maintenance? Yes. Routine inspection and maintenance help ensure reliable long-term performance. A properly designed Tank Safety System is essential for protecting storage tanks, maintaining operational safety and supporting reliable industrial processes. Selecting the right combination of pressure protection devices helps reduce operational risks while improving equipment reliability and process efficiency. ADYAA supplies complete tank safety and pressure protection solutions across Australia, helping industries safeguard storage facilities with reliable, application-specific products. Need help selecting the right Tank Safety System? Our specialists can help you choose the right tank protection solution for your storage application. Tank Safety Systems: Protecting Industrial
What Additional Substances Are Used for Effective Gasket Sealing?
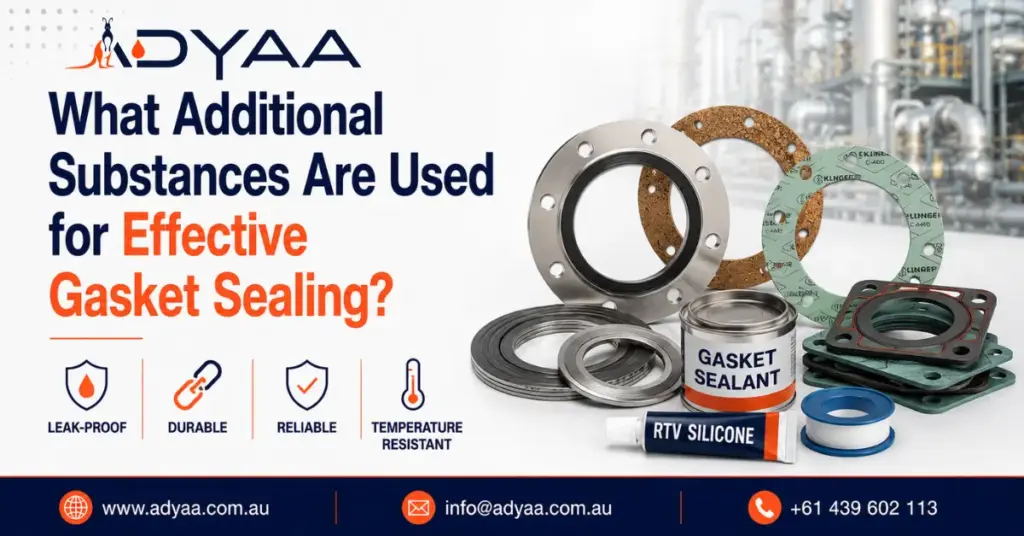
What Additional Substances Are Used for Effective Gasket Sealing? A gasket is designed to seal two mating surfaces and prevent leakage under pressure, temperature and varying process conditions. In many applications, the gasket alone performs exactly as intended. However, certain operating environments demand additional support to maintain a reliable seal over time. The important question isn’t “Which sealant should I use?”—it’s “Does this application actually need one?” Using the wrong sealing compound, applying excessive sealant or relying on additional materials to compensate for poor installation can create more problems than it solves. Understanding where these products fit into gasket sealing helps improve equipment reliability, reduce maintenance and minimise unexpected downtime. When Should Additional Sealing Substances Be Used? Additional sealing products are usually considered when operating conditions place extra stress on the gasket or sealing surface. Common situations include: High operating temperatures High-pressure systems Slightly worn or imperfect flange surfaces Aggressive chemicals Steam applications Frequent equipment maintenance Corrosive environments For example, a chemical processing plant handling aggressive media may require a chemically compatible sealing compound, while a steam pipeline operating at elevated temperatures may benefit from graphite-based lubricants on fasteners to maintain consistent bolt preload. The choice always depends on the process—not simply on the gasket. Common Substances That Support Gasket Sealing Gasket Sealants Gasket sealants are applied as a thin coating to improve contact between the gasket and flange surfaces. They help compensate for minor surface imperfections but should never replace proper flange preparation or correct gasket selection. They are commonly used in: Pumps Gearboxes Compressors Process pipe flanges Applying more sealant does not create a better seal. In many cases, excessive sealant can squeeze into the process line and contaminate equipment. PTFE Tape PTFE tape is one of the most recognised sealing materials, but it is frequently misunderstood. It is intended for threaded pipe connections—not flat gasket faces. Typical applications include: Instrumentation fittings Threaded valves Pipe threads Pneumatic connections Using PTFE tape on flange gasket surfaces is generally not recommended because the gasket is already designed to provide the sealing function. Anti-Seize Compounds Anti-seize compounds are applied to bolts, studs and fasteners rather than the gasket itself. Their purpose is to: Prevent thread galling Reduce corrosion Improve bolt tightening consistency Simplify future maintenance Uniform bolt loading is one of the most important factors in achieving reliable industrial gasket sealing. Graphite Lubricants Graphite lubricants are commonly selected for high-temperature applications where conventional lubricants may degrade or lose their effectiveness. They are widely used in: Boilers Steam systems Thermal processing equipment High-temperature pipework These lubricants help maintain consistent fastening performance during repeated maintenance cycles. Application-Specific Sealing Compounds Certain industries require specialised sealing products designed for specific operating conditions. Examples include: Food-grade sealing compounds Chemical-resistant sealants Oil and gas sealing compounds Pharmaceutical-approved sealing materials Selecting the correct product requires considering the process media, operating temperature, pressure and gasket material. When Additional Sealants Should NOT Be Used One of the biggest misconceptions in industrial maintenance is that adding more sealant automatically improves sealing performance. In reality, additional sealing compounds may be unnecessary when: Flange faces are clean and undamaged. The correct gasket material has been selected. Bolts are tightened correctly. The manufacturer’s installation recommendations are followed. Modern industrial gaskets, including PTFE, graphite and spiral wound gaskets, are often designed to perform without additional sealants. Common Mistakes That Cause Gasket Failure Many sealing failures occur during installation rather than because of the gasket itself. Some of the most common mistakes include: Applying excessive gasket sealant Mixing incompatible sealing compounds Using PTFE tape on flange faces Reusing compressed gaskets Ignoring damaged flange surfaces Uneven bolt tightening Selecting the wrong gasket material Following recognised installation practices, such as ASME PCC-1 bolt tightening guidelines where applicable, can significantly improve sealing reliability. Choosing the Right Sealing Solution Before selecting any additional sealing substance, ask these questions: What fluid is being sealed? Is the media chemically aggressive? What are the operating temperature and pressure? What gasket material is being used? Is the flange surface in good condition? Will the equipment be dismantled regularly? These answers often determine whether the gasket alone is sufficient or whether supporting sealing materials are beneficial. Sealing Material Best Used For Avoid When Gasket Sealant Minor flange imperfections Good flange surfaces with modern gasket materials PTFE Tape Threaded connections Flat gasket joints Anti-Seize Compound Bolts and fasteners Gasket sealing surfaces Graphite Lubricant High-temperature bolting Low-temperature general applications Frequently Asked Questions Can gasket sealant replace a damaged gasket? No. Sealants are designed to support gasket performance, not compensate for damaged or incorrectly selected gaskets. Is PTFE tape suitable for flange connections? Generally no. PTFE tape is intended for threaded fittings rather than gasket sealing surfaces. Can too much gasket sealant cause leaks? Yes. Excess sealant may interfere with gasket compression or enter the process system. Which industries commonly use additional sealing substances? Chemical processing, oil & gas, food manufacturing, pharmaceutical production, power generation and water treatment frequently use specialised sealing products. How can gasket sealing performance be improved? Selecting the correct gasket material, preparing flange surfaces properly, tightening bolts evenly and using additional sealing products only when required provides the most reliable results. Final Thoughts Reliable gasket sealing is rarely achieved by adding more sealing compounds. It begins with selecting the correct gasket material, understanding the operating conditions and following good installation practices. Additional substances such as gasket sealants, PTFE tape, anti-seize compounds and graphite lubricants each have a specific purpose. When selected correctly, they help improve sealing performance and reduce maintenance. When used incorrectly, they can create unnecessary reliability issues. Rather than treating every application the same, evaluate the process conditions, media compatibility and equipment design before deciding whether additional sealing materials are required. Industrial facilities handling demanding process conditions often benefit from using high-quality industrial gaskets, compatible sealing solutions and correctly selected instrumentation to improve long-term equipment reliability. ADYAA supports industries across Australia with a comprehensive range of industrial sealing products, helping maintenance teams and engineers choose solutions that match their application rather
What Is Industrial Sealing and Why Is It Important?
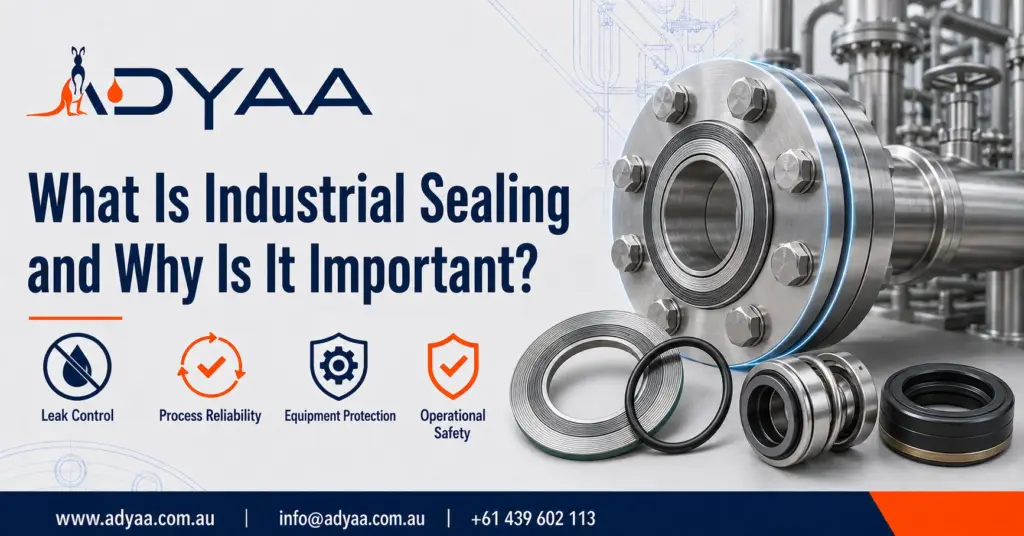
What Is Industrial Sealing and Why Is It Important? In a massive refinery or a high-pressure mining plant, the most critical component often isn’t the largest pump or the tallest reactor—it’s the smallest seal. Industrial sealing is the unsung hero of process integrity. Whether it is a Ring Type Joint (RTJ) gasket in an oil pipeline or a simple O-ring in a hydraulic cylinder, seals are the barrier between a safe, efficient operation and a catastrophic failure. We specialize in high-performance sealing solutions for Australia’s toughest environments. In this guide, we break down what industrial sealing actually is, why it is critical for your bottom line, and the different types you need to know about. Industrial Sealing Solutions for Maintenance Managers, Process Engineers and Procurement Officers in Oil & Gas/Mining. What Is Industrial Sealing? At its core, industrial sealing is the technology used to block the passage of fluids (liquids or gases) through the gap between two joined surfaces. It serves two primary functions: Containment: Keeping the internal media (oil, steam, acid) inside the system. Exclusion: Keeping external contaminants (dust, dirt, moisture) outside the system. While this sounds simple, the challenge lies in the conditions. Industrial seals must maintain this barrier while enduring extreme temperatures (from cryogenic -196°C to scorching +1000°C), massive pressures (up to 20,000 PSI), and aggressive chemical corrosion. Why Is Industrial Sealing Important? You might view seals as cheap consumables, but their failure can cost millions. Here is why investing in quality sealing (like ADYAA’s RX Rings or Spiral Wound Gaskets) is non-negotiable. 1. Safety and Hazard Prevention The most immediate importance of sealing is human safety. In industries like Oil & Gas, a leaking flange isn’t just a mess; it’s a fire hazard or a toxic cloud. Proper sealing ensures that volatile organic compounds (VOCs) and dangerous chemicals stay contained, protecting your workforce from exposure and explosions. 2. Operational Efficiency A system that leaks pressure is a system that bleeds money. Pneumatic systems: Leaking air forces compressors to work harder, driving up electricity bills. Hydraulic systems: Fluid loss results in sluggish machinery and reduced force. High-quality seals ensure your equipment runs at peak parameter settings without wasting energy. 3. Environmental Compliance Australia has strict environmental regulations regarding emissions and ground contamination. A reliable sealing system helps you meet EPA standards by preventing “fugitive emissions”—the slow, invisible leaks of gas from valves and flanges that can lead to heavy fines. 4. Equipment Longevity Seals act as the first line of defense for your expensive assets. For example, a Spring-Energized Seal or a Polymer Bellow protects internal bearings and shafts from grit and corrosion. If the seal fails, contaminants can enter the equipment, accelerating wear and potentially causing premature component failure. Types of Industrial Sealing Solutions Not all seals are created equal. Depending on your application, you will generally rely on one of these categories: A. Static Seals (Gaskets) These are used between two stationary surfaces, such as pipe flanges. RTJ Gaskets (Ring Type Joints): Metal gaskets (Oval, Octagonal, RX, BX) designed for high-pressure/high-temperature applications. They form a metal-to-metal seal ideal for the Oil & Gas industry. Spiral Wound Gaskets: A mix of metal winding and soft filler (graphite/PTFE), offering excellent recovery for fluctuating temperatures. B. Dynamic Seals These seals are between parts that move relative to each other (like a piston rod or a rotating shaft). Spring-Energized Seals: Used when standard elastomers fail. A spring ensures constant contact while maintaining sealing force as the sealing interface changes. Packing: Soft braided material compressed around a shaft to prevent leakage in pumps and valves. C. O-Rings One of the most widely used seal types, O-rings are donut-shaped loops that sit in a groove and compress to prevent fluid leakage. Elastomeric: NBR, Viton® (FKM), or EPDM, selected for suitable operating conditions. Metal O-Rings: Used by ADYAA for extreme environments, such as aerospace and cryogenic applications, where conventional rubber seals may not withstand the operating conditions. Summary: Don’t Let a Leak Stop Your Plant A seal might cost $50, but it protects a $500,000 pump and ensures the safety of everyone on site. Whether you need standard Lens Rings for steam lines or custom CNC-machined sealing components, quality matters. ADYAA supplies a full range of gaskets, O-rings, and custom seals engineered for the Australian industry. Need help selecting the right material for your chemical plant? View Our Full Range of Sealing Solutions. Contact our engineers for a consultation. What Is Industrial Sealing and Why Is It Important? Pressure Instrumentation Suppliers: What to Look for Before You Buy Selecting a pressure instrument isn’t simply about finding the lowest… Read More → Pressure Instrumentation Suppliers: What to Look for Before You Buy. Pressure Instrumentation Suppliers: What to Look for Before You Buy Selecting a pressure instrument isn’t simply about finding the lowest… Read More → The Role of Sealing in Preventing Leakage and Safety Hazards Focus The Role of Sealing in Preventing Leakage and Safety Hazards A leak is rarely just a “drip.” In a chemical… Read More →